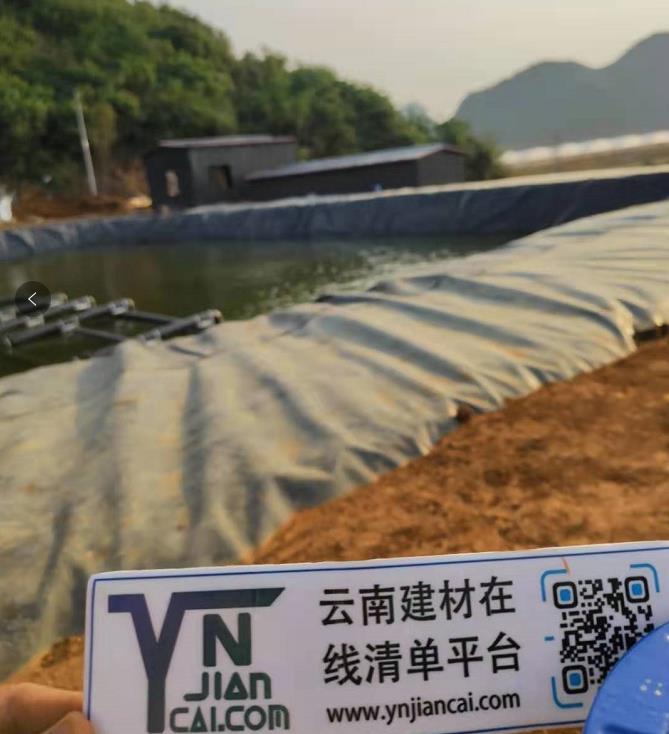
Laying of HDPE impermeable membrane geomembrane
1. Before laying HDPE geomembrane, there should be corresponding qualified acceptance certification documents for civil engineering.
2. Before cutting HDPE membrane, relevant dimensions should be accurately measured, then cut according to actual conditions. Generally, it is not advisable to cut according to the dimensions shown in the diagram. Each piece should be numbered and recorded in detail on a special form.
3. When laying HDPE geomembrane, strive to minimize welds, and save raw materials as much as possible under the premise of ensuring quality. At the same time, it is also easy to ensure quality.
4. The lap width of joints between membranes is generally not less than 10cm, usually making the weld arrangement direction parallel to the maximum slope, that is, arranged along the slope direction.
5. Usually at corners and deformed sections, the joint length should be shortened as much as possible. Except for special requirements, on slopes with a gradient greater than 1:6, within 1.5 meters from the top slope or stress concentration area, try not to set welds.
6. During the laying of HDPE geomembrane, avoid artificial wrinkles. When the temperature is low, try totighten and flatten.
7. After the HDPE geomembrane is laid, minimize walking on the membrane surface, moving tools, etc. Any objects that can cause harm to the HDPE membrane should not be placed on the membrane or carried while walking on the membrane, to avoid accidental damage to the membrane.
Composite geomembrane construction scheme II
Welding of composite geomembrane
1. The welding process of hot wedge welding machine is divided into: adjust pressure, set temperature, set speed, weld lap inspection, load membrane into machine, start motor, pressurize welding.
2. There should be no oil or dust at the joints, and the lap section of HDPE geomembrane should not contain debris such as sediment. When there is debris, it must be cleaned before welding.
3. At the beginning of welding every day, a 0.9mm×0.3mm sample must be trial-welded on site first, with a lap width of not less than 10cm, and a tensile machine is used for on-site peeling and shear tests. After the sample is qualified, formal welding can be carried out with the speed, pressure and temperature adjusted at that time. The date, time, and ambient temperature must be marked on the sample. During the welding process of the hot wedge welding machine, pay attention to the operation of the welding machine at any time, and make fine adjustments to speed and temperature according to the actual situation on site.
4. Welds are required to be neat and beautiful, and there must be no slip welding or skip phenomena.
5. When the geomembrane length is insufficient, longitudinal splicing is required. The transverse welds should be welded first, then the longitudinal welds. Transverse welds separated by more than 50cm should be T-shaped, not cross-shaped.
6. Adjacent geomembrane welds should be staggered as much as possible. The nodes formed between membrane blocks should be T-shaped, minimize cross-shaped, and the intersections of longitudinal and transverse welds should be strengthened with an extrusion welding machine.
7. When welding membranes, dead folds must not be pressed out. When laying HDPE geomembrane, according to the local temperature change range and HDPE geomembrane performance requirements, reserve the expansion and contraction deformation caused by temperature changes.
8. When the welding machine temperature indicated by the temperature control of the portable welding machine is lower than 200℃, use a clean cloth or cotton yarn to wipe off before welding. If necessary, re-grind, do not wipe by hand.
9. When there is condensation, moisture, sediment, etc. at the joints affecting welding, treat before welding.
10. Welding cannot be carried out during rain or when there is moisture, dew, or heavy sand at the joints, except when protective measures are taken.
11. When the temperature is lower than 5℃, construction should not be carried out according to specification requirements. If construction must be carried out, the welding machine should be preheated before welding.
12. During the welding process of the extrusion welding machine, the slider of the gun head should be checked frequently. When wear is serious, replace the slider in time to avoid damaging the membrane surface.
13. When welding geomembrane, a generator with good voltage stabilization performance should be used for power supply. In special cases, when using local electricity, a voltage stabilizer must be used.

 " />
 English