
 " />
【 WeChat QR code consultation】
+86 13698775878
Air pressure testing verifies the integrity of double-track hot wedge welds before covering the liner.
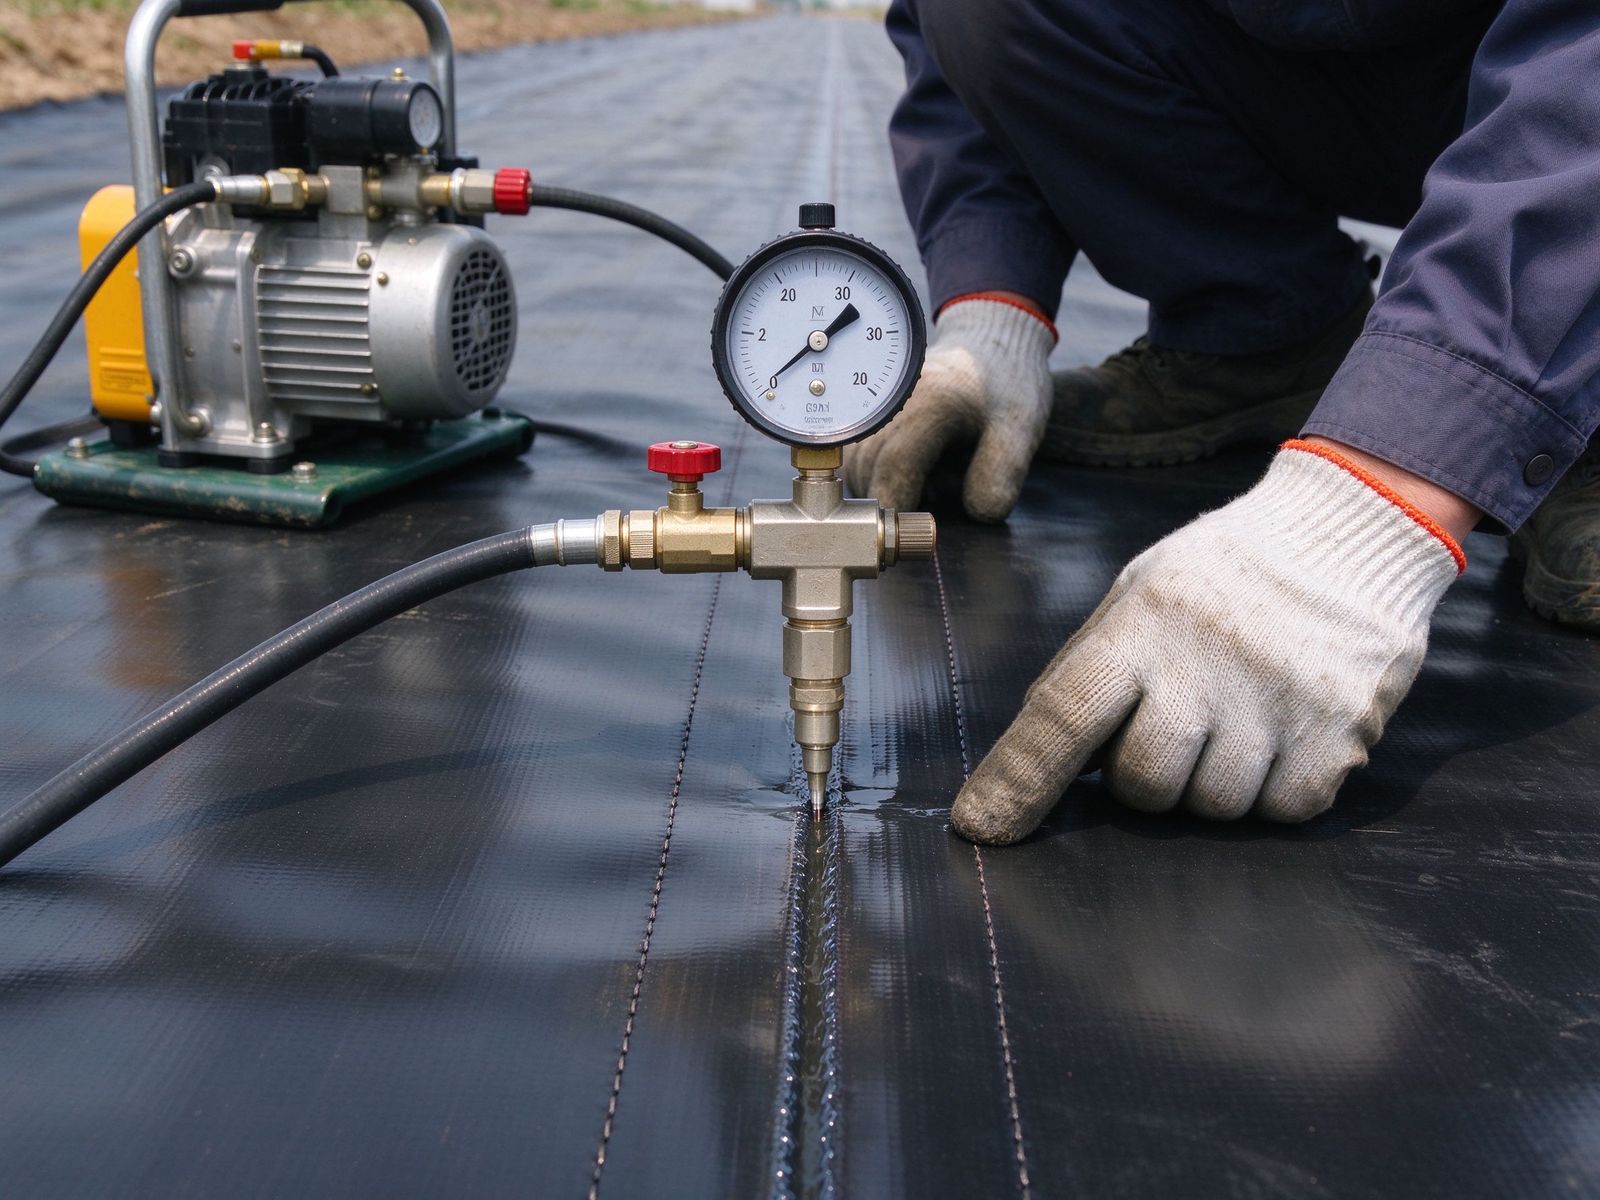
Insert a test probe into the unwelded channel at both ends of the seam. Plug one end and pump air into the other with a hand pump. Hold the prescribed pressure for the required time. A steady gauge confirms a sound seam.
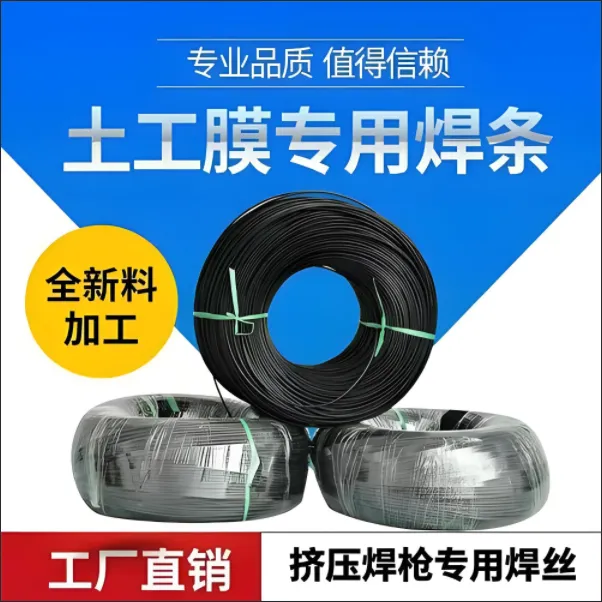
We supply geomembrane and welding rod. Contact us for technical support.
Scan code consultation
 English